South Africa has stringent regulations on the transport and storage of pharmaceutical products, aimed at ensuring safety and product integrity throughout the supply chain. Manufacturers, chemical suppliers and distributors that handle bulk active pharmaceutical ingredients (APIs) must choose the right packaging products to meet regulatory compliance guidelines.
The South African Health Products Regulatory Authority (SAHPRA) regulates the distribution and packaging of pharmaceuticals in the country, in accordance with the Medicines and Related Substances Act (Act 101 of 1965). All bulk handling and transport procedures should be carried out following strict quality standards.
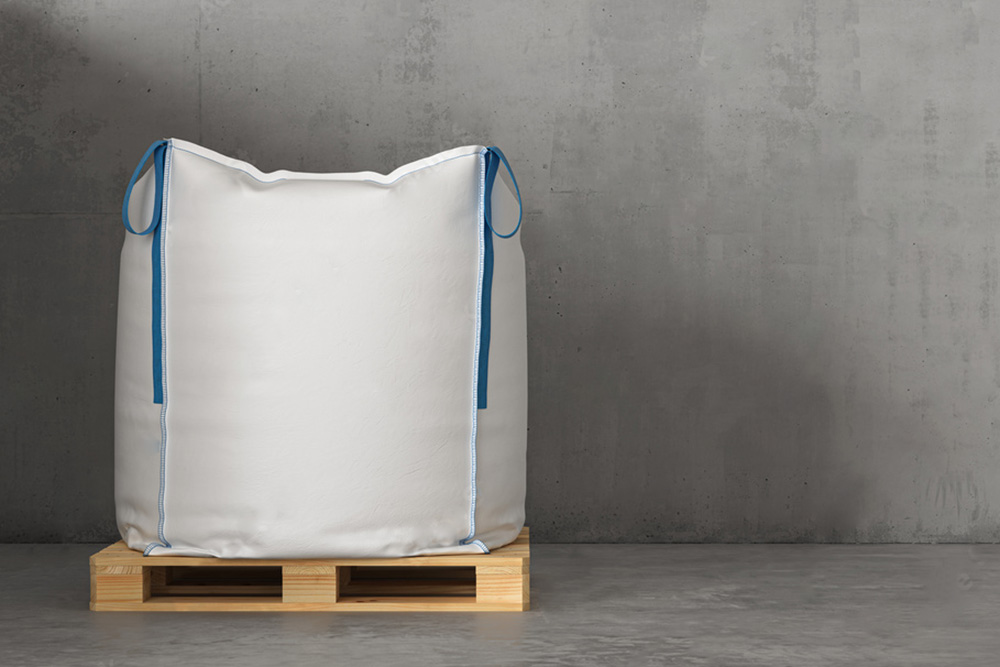
Custom Bulk Bags (CBB) has recently installed a food-grade manufacturing facility in its productsion line. We can produce up to 3.5 million flexible intermediate bulk containers (FIBCs), also known as bulk bags, every year for pharmaceutical processors in South Africa and neighbouring countries. These flexible woven containers can store up to two tonnes of goods per bag.
Regulations on pharmaceutical packaging
SAHPRA enforces strict Good Manufacturing Practice (GMP) & Good Distribution Practice (GDP) guidelines requiring all primary, secondary and tertiary packaging to prevent contamination, degradation or exposure to moisture during transit.
Containers for bulk APIs, binders and dry pharmaceutical inputs are required to meet food-grade and pharmaceutical-grade cleanliness standards. Packaging must be produced from 100% virgin polypropylene (PP) in cleanroom facilities (compliant to ISO 14644 or ISO 22000 / HACCP systems) so that no microscopic particles, oils or foreign contaminants enter the batch.
SAHPRA’s newly updated health product traceability framework requires that tertiary packaging (such as bulk bags and pallets) need to be able to support standardised identification including GS1 compliant batch/lot numbers and Global Trade Item Numbers (GTINs) for full supply chain visibility.
Dry pharmaceutical powders and fine granulates are highly sensitive to the build-up of static electricity during high-speed filling and emptying. In the presence of combustible dust, anti-static or groundable bulk bags are required to remove the risk of explosion as dictated by regulations.
Some active raw materials and intermediate chemical compounds are classified as dangerous goods. The packaging used for these materials must be internationally UN-certified to prove that it can withstand physical drops, stacking pressures and tear forces in transit.
Bulk bags make pharmaceutical operations more efficient
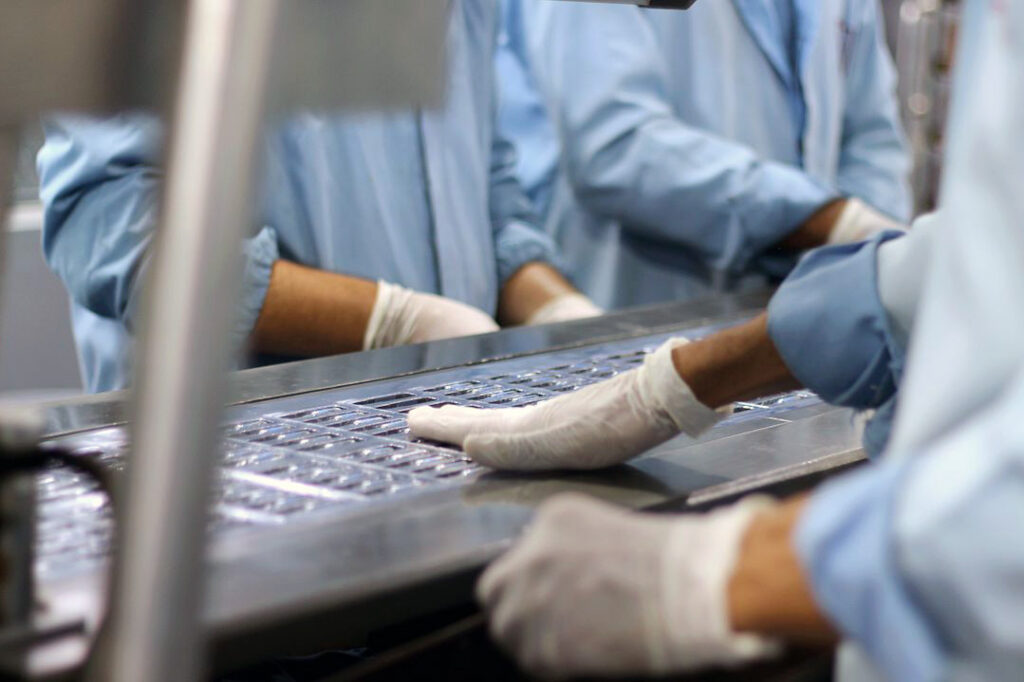
FIBCs play an important role in modern pharmaceutical manufacturing and provide a safe and hygienic connection between raw chemical production, processing plants and distribution centres. Here are some of the ways in which FIBCs can be used in the pharmaceutical supply chain:
- Powder transfer in manufacturing facilities – Transporting bulk volumes of powdered substances, such as lactose, starch and APIs, from storage bays to mixing, granulation or tabletting equipment. They help to contain dust thanks to sift-proof seams and sealed spout tops and bottoms.
- Inter-facility logistics – Moving bulk quantities of raw materials between chemical synthesis plants and secondary formulation facilities. FIBCs offer high volume-to-weight ratios, stackability and collapsibility, which all optimise space. These bags can be customised to integrate with industrial hoppers and blenders, which improves precision and reduces spillage.
- Distribution centre storage – FIBCs are perfect for storing bulk excipients and active intermediates in distribution centres, prior to secondary packaging. Specialised inner liners can protect hydroscopic ingredients from moisture, humidity and oxygen.
South Africa’s premier supplier of pharma-grade FIBCs
CBB is a top South African manufacturer of premium FIBCs, providing engineered bulk packaging designed to meet the strict requirements of the pharmaceutical industry. With an annual output of up to 3.5 million bags, we guarantee local supply chain stability, fast turnaround times and compliance with national and international standards.
Our pharma-grade and food-grade bulk bags are manufactured under strict hygienic conditions, using 100% virgin woven polypropylene to prevent chemical leaching and contamination risks. We work directly with clients to create custom FIBC solutions tailored to their specific machinery and material properties.
CBB has a modern cleanroom production line, so we can manufacture bulk bags in ultra-clean environments and fit them with low-density polyethylene (LDPE), EVOH barrier, or aluminium foil liners for humidity-sensitive powders. We can also make fully groundable Type C bags with conductive threads, or self-dissipating Type D anti-static fabrics to safely handle combustible dusts and flammable solvents without static discharge.
Our bulk bags are tested and certified to UN standards, with Safety Factors of 5:1 (single-trip) or 6:1 (multi-trip/heavy-duty), capable of carrying up to 2000kg safely. Working with CBB helps to keep your pharmaceutical supply chain compliant, efficient and protected. Please contact us today to chat with our sales team about our bulk bag offerings.
___
Custom Bulk Bags is a major South African manufacturer of woven polypropylene bags for various industries, including mining, chemicals and agriculture. We are a Level 1 B-BBEE supplier that falls under the ownership structure of Deneb Investments Limited. For more information on our products, contact sales@custombulkbags.co.za.
